
- 713.590.1312
- sale@pandbtools.com
What Is a Copper Busbar Extrusion Machine?
Copper Busbar Extrusion Machine technology sits at an important point between copper processing and modern electrification. It converts heated copper billets into continuous, accurately shaped bars. These bars carry electricity inside switchgear, transformers, battery systems, data centers, and renewable-energy equipment. The process must control temperature, die wear, dimensional tolerance, and surface quality. A small defect can create a costly installation problem.
Demand pressure is increasing. The International Energy Agency’s Global Critical Minerals Outlook 2024 estimates that copper demand may rise from approximately 26 million metric tons in 2023 to about 31 million metric tons by 2035 under its Stated Policies Scenario. S&P Global’s 2024 copper study also warns of a potential supply gap as electrification expands. These figures do not guarantee growth for every equipment supplier. They do show why efficient forming deserves closer attention.
Professor John G. Lenard, a recognized metal-forming authority, defines the basic principle clearly: “Extrusion is a process in which a billet is forced through a die.” That simple sentence hides difficult engineering choices. A modern Copper Busbar Extrusion Machine needs stable hydraulic pressure, precise cooling, automatic length control, and dependable measurement systems. Operators still matter. No machine is perfect. Poor billet preparation, unnoticed die damage, or incorrect alignment can reduce conductivity and increase scrap. The strongest evaluations therefore examine real output, energy use, maintenance access, and repeatability—not impressive brochures alone.
What a Copper Busbar Extrusion Machine Does and Why It Matters
What Is a Copper Busbar Extrusion Machine?
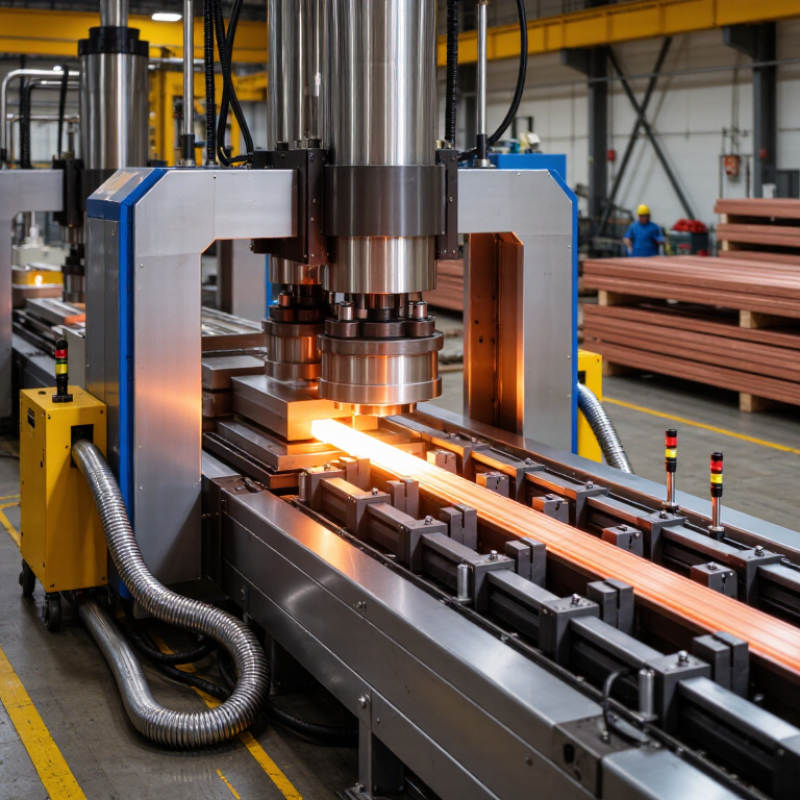
A copper busbar extrusion machine converts heated copper billets into precise, continuous electrical conductors. The billet enters a container and moves through a hardened die. Pressure shapes it into a flat bar, hollow section, or custom profile. Water cooling then stabilizes the dimensions before cutting, straightening, and inspection.
The process matters because busbars carry high currents inside switchgear, battery systems, transformers, and data-center equipment. A small thickness error can create poor contact, uneven heating, or difficult assembly. Good extrusion control reduces scrap and keeps edges cleaner. It also supports consistent conductivity across long production runs.
Practical experience shows that die alignment and cooling speed deserve close attention. They are easy to underestimate.
Industry demand gives this equipment wider importance. The International Energy Agency’s Global Critical Minerals Outlook 2024 projects total copper demand rising from about 26 million tonnes in 2023 to over 31 million tonnes by 2035. The report also expects clean-energy copper demand to grow substantially during that period. The International Copper Study Group reported global refined copper usage near 26 million tonnes in 2023. These figures suggest stronger pressure on productivity, material efficiency, and repeatable quality.
Not every extrusion line performs equally.
Higher speed is not automatically better. Operators still need to balance billet temperature, extrusion pressure, die wear, and surface finish. That judgment remains partly practical, and sometimes imperfect. A reliable machine is valuable because it makes those variables visible, measurable, and easier to correct.
Copper Grades, 99.9% Purity, and 58 MS/m Conductivity Requirements
What Is a Copper Busbar Extrusion Machine?
A copper busbar extrusion machine forces a heated copper billet through a precision die. It creates flat, rigid conductors with consistent width, thickness, and corner radii. The selected copper grade controls electrical and processing performance.
C11000 copper usually contains at least 99.90% copper, according to Copper Development Association alloy data. Its conductivity is commonly near 100% IACS. IEC 60028 defines standard annealed copper at about 58 MS/m at 20°C. This value is a useful production benchmark, not an automatic guarantee. Impurities, excessive heating, and poor cooling can reduce conductivity.
Some applications specify oxygen-free copper, such as C10200, when welding or thermal stability matters. However, higher purity can increase material cost and may not improve every busbar design. That assumption deserves review. A reliable extrusion line controls billet temperature, extrusion speed, die wear, and post-extrusion cooling. Small dimensional errors can create hot spots at bolted joints.
USGS Mineral Commodity Summaries 2025 identifies copper as essential for electrical equipment and power infrastructure. This demand makes traceable quality control increasingly important. Manufacturers should verify chemical composition, conductivity, tensile strength, and cross-sectional dimensions for each production lot. A conductivity meter, calibrated properly, can reveal problems that visual inspection misses. Yet testing only finished bars is imperfect; process records remain equally important.
Core Machine Systems: Billet Heater, 8–12 MN Press, Die, and Puller
What Is a Copper Busbar Extrusion Machine?
A copper busbar extrusion machine forms heated billets into long, conductive profiles. Its core systems work as one controlled production line. The billet heater raises copper to a suitable forming temperature without creating excessive surface oxidation. Temperature consistency matters. A cold billet increases press load, while an overheated billet may damage the die or reduce dimensional control. In practice, operators should verify billet temperature at several points, not trust one display.
The 8–12 MN extrusion press supplies the force needed to push copper through a shaped die. This press typically includes a container, stem, hydraulic system, and monitoring controls. Pressure changes can reveal poor lubrication, incorrect heating, or a partially blocked die.
The die defines the busbar width, thickness, holes, and edge profile. Small wear can change tolerances. That detail is easy to underestimate.
After extrusion, the puller grips the emerging bar and maintains steady movement. Its speed must match metal flow from the press. If it pulls too quickly, the profile may stretch or become undersized. If it moves unevenly, surface marks and dimensional variation can appear. Cooling equipment, guides, and measurement tools support this stage. I have found that clean alignment often matters as much as rated press capacity. A powerful machine still produces inconsistent busbars when guides are poorly adjusted. Manufacturers should record temperature, pressure, speed, and profile measurements for each production run.
Step-by-Step Extrusion at Approximately 650–950°C for Precise Profiles
What Is a Copper Busbar Extrusion Machine?
A copper busbar extrusion machine converts heated copper billets into long, accurately shaped conductors. The process usually begins with billet inspection, cutting, and controlled heating. Temperatures commonly range from approximately 650–950°C, depending on copper grade, profile complexity, and equipment design. This range is useful, but it is not a magic setting.
The heated billet enters a container, where a hydraulic ram pushes it through a precision die. Copper flows continuously, forming a flat bar, channel, or custom electrical profile. Operators monitor ram pressure, billet temperature, extrusion speed, and die wear. Small changes can affect surface finish and dimensional accuracy. After leaving the die, the profile is cooled, straightened, cut, and inspected for cracks, twists, and thickness variation. Water cooling is not always ideal; excessive cooling may increase distortion.
Demand explains the attention given to this equipment. The IEA’s Global Critical Minerals Outlook 2024 indicates that clean-energy copper demand could grow from roughly 6 million metric tons in 2023 to more than 10 million by 2035, depending on the scenario. The USGS Mineral Commodity Summaries 2024 reported global mined copper production near 22 million metric tons in 2023. These figures suggest pressure for efficient processing. Still, production speed should not replace inspection. A profile may look smooth while hiding internal stress or uneven conductivity. Experienced operators often adjust settings during a run, because real copper rarely behaves as perfectly as a textbook billet.
Dimensional Tolerances, Surface Quality, and Electrical Testing of Busbars
What Is a Copper Busbar Extrusion Machine?
Dimensional Tolerances, Surface Quality, and Electrical Testing of Busbars
A copper busbar extrusion machine forces heated copper through a shaped die. The process creates continuous bars with controlled width, thickness, and profile. Dimensional tolerance is not a single number. It depends on alloy, extrusion temperature, die wear, cooling, and straightening. Inspectors commonly measure thickness and width with calibrated micrometers. They also check twist, bow, corner radius, and cut length. A small thickness change can affect installation clearance and heat dissipation.
Surface quality needs close visual and mechanical inspection. Scratches, die lines, cracks, pits, and oxidation may appear after extrusion. Some marks are cosmetic, while others can increase contact resistance. A clean surface can still hide a problem. Light-angle inspection often reveals fine longitudinal lines. Surface roughness testing may support visual checks, especially on contact faces. Protective handling matters because copper edges can be damaged during cutting, stacking, or transport.
Electrical testing confirms whether the busbar performs beyond its appearance. Four-wire resistance measurements can identify conductivity changes with greater accuracy. Technicians may also calculate resistivity after recording length, cross-sectional area, and temperature. Temperature correction is essential because copper resistance rises as temperature increases. Test instruments require calibration and traceable records. One practical weakness is relying on one test point. Resistance can vary along a bar, so repeated measurements provide stronger evidence. Even then, results should be reviewed against the project specification, not assumed acceptable.